If you’ve never watched an inspection, the process can feel like a black box. A report arrives, it says pass or fail, and you take it on trust. Knowing what the inspector actually does on the day helps you write a better brief, read the report more critically, and spot a visit that was cut short. This is how a typical pre-shipment inspection in India runs, from the factory gate onwards.
Timing comes first. The inspection normally takes place when production is complete and most of the goods are packed, commonly at least 80 percent. Too early and the inspector can’t pull a representative sample from finished cartons. Too late and the goods are already loaded, which makes rework painful. Confirm the date with the factory a few days ahead and share the inspector’s name and phone number so that nobody is waiting at reception.
The visit opens with a short meeting. The inspector introduces themselves, confirms the purchase order number, the product, the quantity, and the approved sample, and asks the factory to show the finished goods. At this point they check that the quantity produced and the quantity packed match what you were told. A shortfall found here is useful information, because it explains why a shipping date may slip.
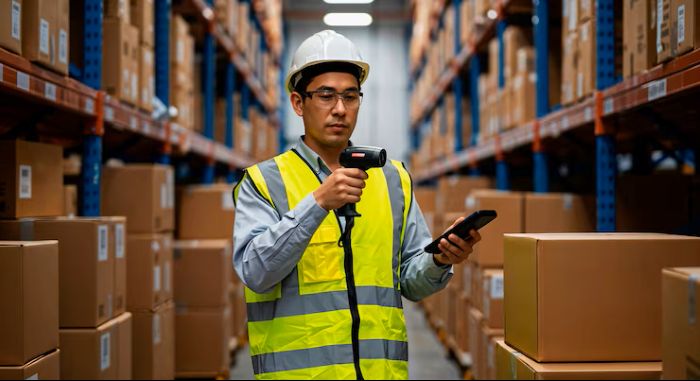
Random carton selection is the step buyers most want to understand. The inspector picks cartons from across the whole lot, not from a stack the factory has set aside near the door. Wherever the goods sit in the warehouse, they choose cartons from different pallets and different heights. Using the AQL table, they work out the sample size for the lot, say 200 units for a lot of around 5,000, and draw units from the selected cartons. Factories that pre-select cartons are a known issue, and a good inspector watches for it.
Next comes the product check itself, which is the core of quality control inspection in India, run against your checklist. For each sampled unit the inspector looks at appearance, workmanship, dimensions, weight, labelling, and any function that applies to the product. Measurements are taken with calibrated tools and compared to the specification. Defects are photographed and classified as critical, major, or minor, and tallied against the acceptance numbers for the chosen AQL level. If the number of major defects exceeds the limit, the lot fails, regardless of how good the rest looks.
Packaging and marking get their own check. The inspector confirms that the carton labels, barcodes, shipping marks, and inner packaging match your instructions. Many carton drop tests are done on the spot: a packed carton is dropped from a set height onto its corners, edges, and faces, then opened to see whether the contents survived. Damage found here usually points to weak inner packaging, and it is far cheaper to fix before loading than after delivery.
Conditions in India can affect the visit in ways worth planning for. Power interruptions can halt function testing, so ask the factory to confirm that a generator or backup supply is available. Inspection areas should have enough light to see surface defects. For products that need testing equipment, such as a meter or a gauge, confirm in advance whether the inspector brings their own or uses the factory’s calibrated tools.
When the checks are done, the inspector holds a closing meeting. They summarise the findings, show the main defects, and ask the factory representative to sign the report. A signature doesn’t mean the factory agrees with the result, only that the findings were presented. If the factory disputes something, the disagreement is noted in the report, and photos back up the inspector’s position.
The result then falls to you. A pass means the goods can ship. A fail gives you options: ask the factory to sort and rework the lot, then re-inspect, or negotiate a discount, or reject the shipment. Agree in advance who pays for a re-inspection, because it’s easier to settle before the factory is under pressure. Providers like InspectionService.com arrange these inspections across India’s main manufacturing regions, and the report format includes the photos and defect counts you need to make the call.
The more precise your brief, the better the visit goes. Send the approved sample, the specification, the label artwork, and a list of the defects that worry you most. An inspector with that material can spend the day checking what matters to you instead of working from a generic form.